Pneumatic Vacuums For every hazardous area and wet cleanup duty.
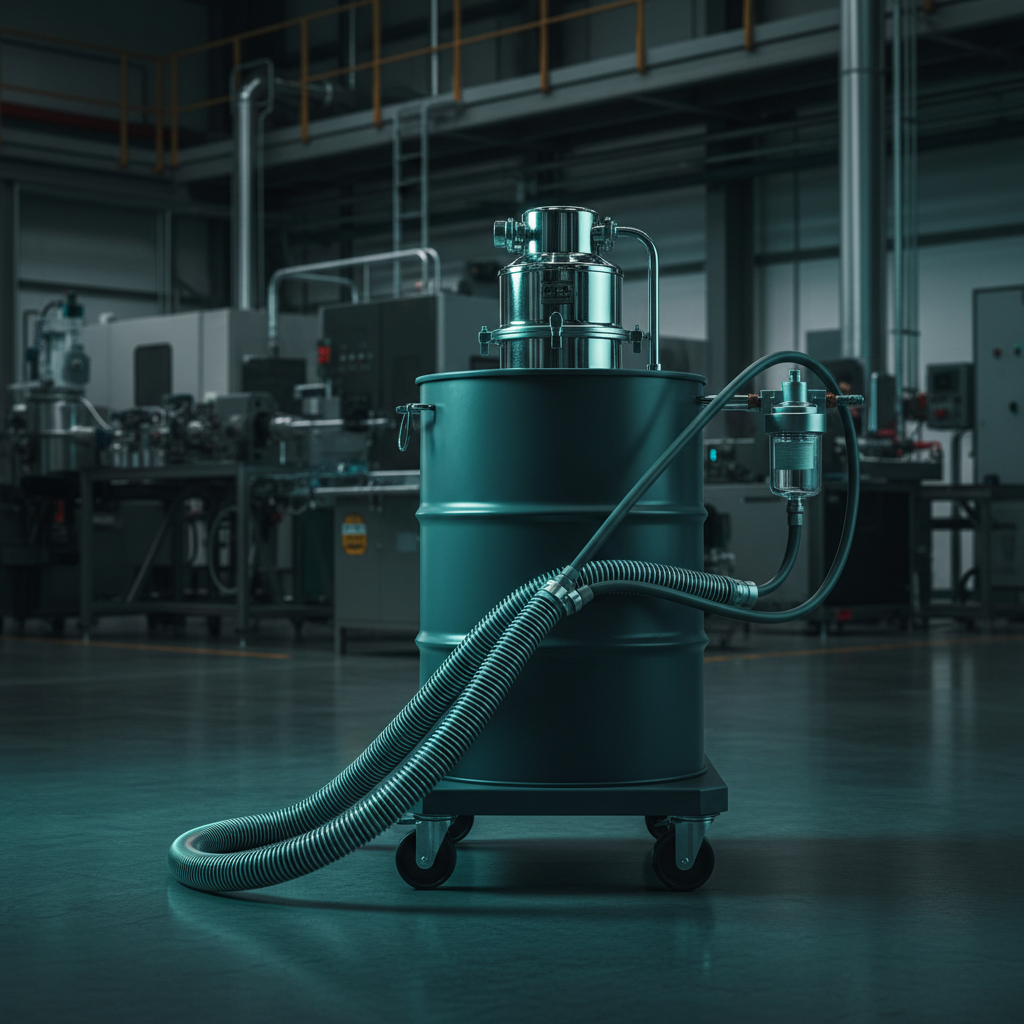
Heavy-duty pneumatic vacuums for chemical and petrochemical plants, pharmaceutical powder handling, food and grain processing, and metalworking shops. Compressed air through a venturi head eliminates the electric motor, prevents overheating, and leaves the power head with no moving parts to wear.
A venturi handles all the work, meaning no electrical components are present at the vacuum unit.
60 to 100 psi
Typical supply pressure with consumption in tens of SCFM.
Continuous duty
Since nothing within the power head generates heat, runtime has no thermal limit.
The fundamentals
How a Pneumatic Vacuum Works
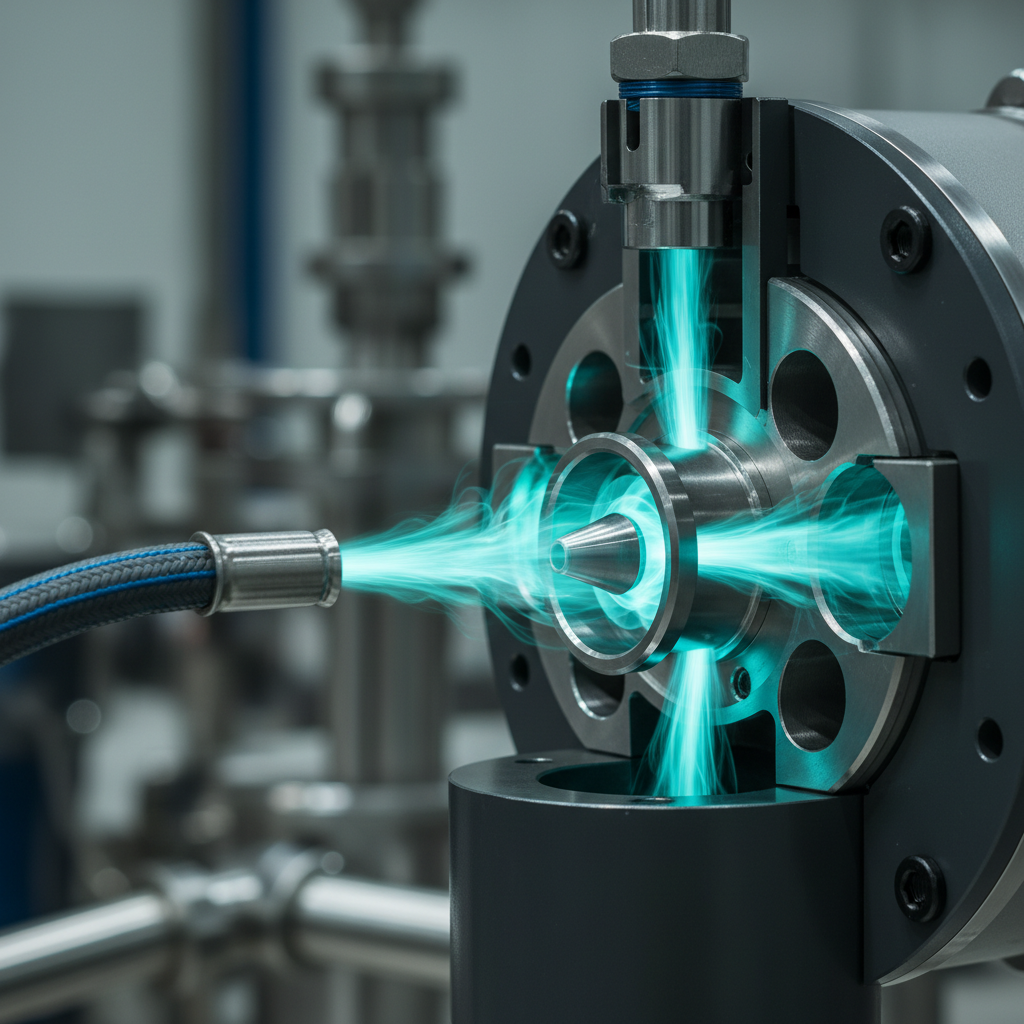
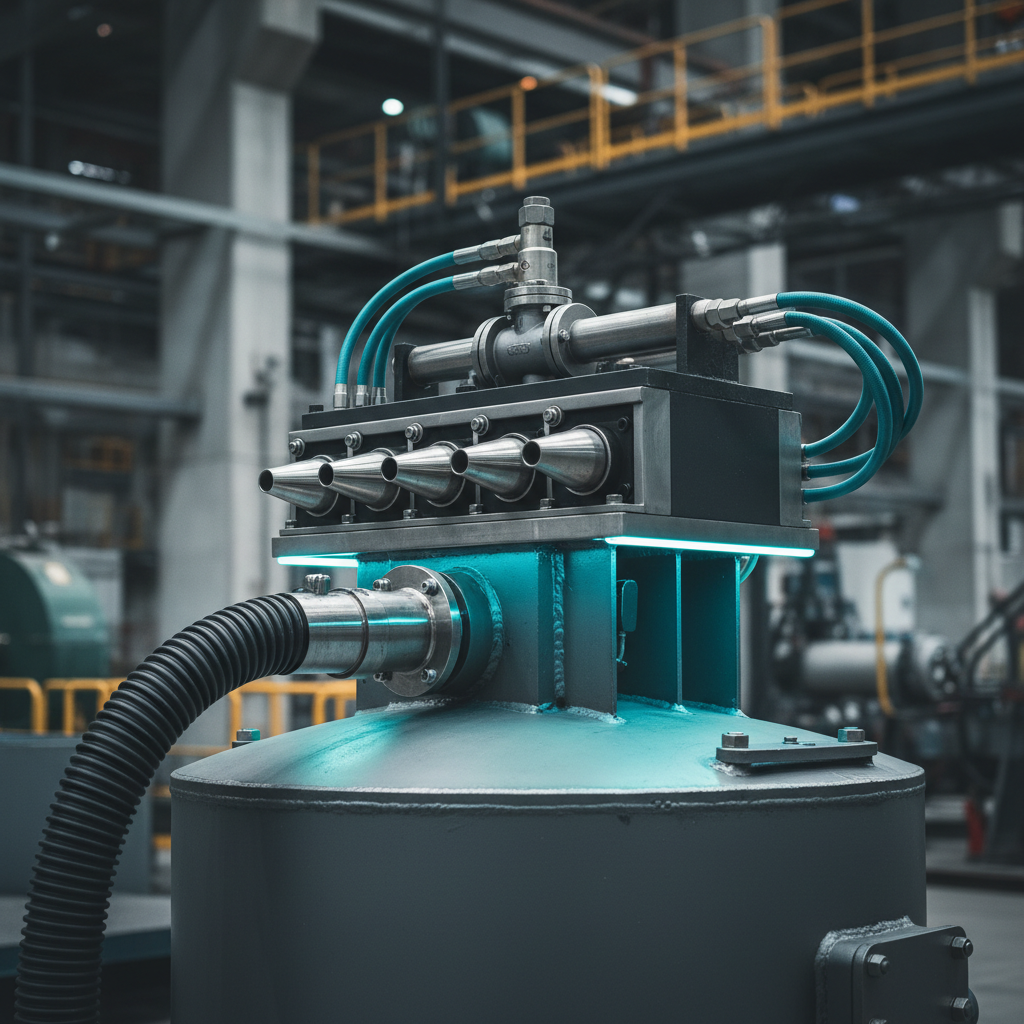
Compressed air flows to the power head and passes through a converging nozzle inside a larger throat. The high-velocity jet drags surrounding air along and exhausts it, creating the venturi effect; that's the entire mechanism.
Pulling air from a sealed vessel faster than leakage creates a partial vacuum. Atmospheric pressure then pushes air and material up the hose. The machine doesn't suck; it removes air, and the atmosphere lifts. That distinction explains much behavior, including why a bad lid gasket mimics a worn vacuum.
With no armature, bearings, or fan, the power head has nothing to overheat, stall, or wear, and no electricity. That's why these units are chosen wherever an electric motor is a liability: classified areas with flammable vapor or combustible dust, wet and washdown work, and continuous shift or turnaround duties. The principle dates to Venturi's late-1700s description; air and steam ejectors built on it remain standard industrial hardware.
Venturi Power Head
Compressed air speeds through a converging nozzle into a larger throat, entraining surrounding air and exhausting it to pull a vacuum. No part rotates, reciprocates, or wears.
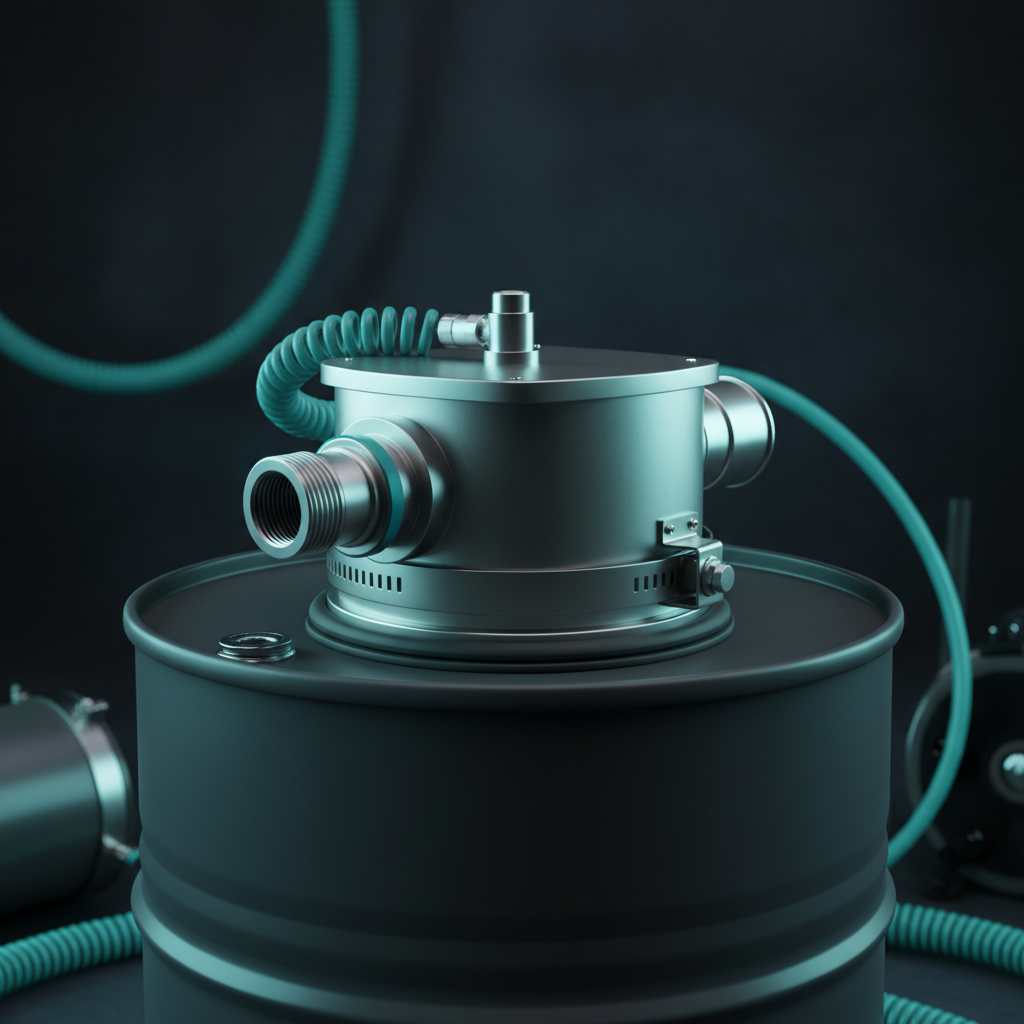
Vessel and Lid Seal
Most heads clamp directly to a 30 or 55 gallon steel drum with a band clamp and lid gasket. The gasket seals the vessel; a flattened or missing one makes the machine appear weak at the hose.
Filtration Stack
Exhaust air passes through a cloth bag, pleated cartridge, or cartridge plus HEPA final stage, chosen by material fineness and discharge location. Filtration controls what stays in the drum and the airflow reaching the hose.
Air, Muffler, and Grounding
A filter-regulator provides clean dry air at rated pressure, the muffler reduces jet noise, and conductive hose with a bonding strap drains static to earth. For combustible dust, these are mandatory specification items.
Where Suction Comes From
Three consequences arise from atmosphere doing the pushing. First, the vessel must seal: a flattened gasket, dented rim, or loose band clamp costs more performance than a worn venturi. Second, supply pressure is mandatory. A head rated 80 psi fed at 50 loses lift and airflow; the air line is at fault. Third, every hose foot and bend subtracts performance, so a long run needs a larger bore and higher-lift head, not just a longer hose on the same unit.
The line-up
Pneumatic Vacuum Types and Differences
Every unit works the same: compressed air through a venturi, sealed vessel, filtration, and hose. Differences lie in venturi count, vessel type, liquid capability, and whether the operator carries or wheels the unit.
Drum-mounted venturi heads
The workhorse. One venturi head clamps onto a standard 30 or 55 gallon drum, turning the drum into the vessel. It lifts by hand, costs a fraction of a complete unit, and when full, you swap drums. Most plants keep one head and several drums.
Since it mates with commonplace 30-gallon and 55-gallon drums, the container you need likely already sits on your floor.
The head weighs little, lacks a motor, and can be shifted effortlessly from zone to zone and cleaned with minimal hassle.
Exchange a filled drum with an empty unit rather than opening and cleaning an onboard machine vessel.
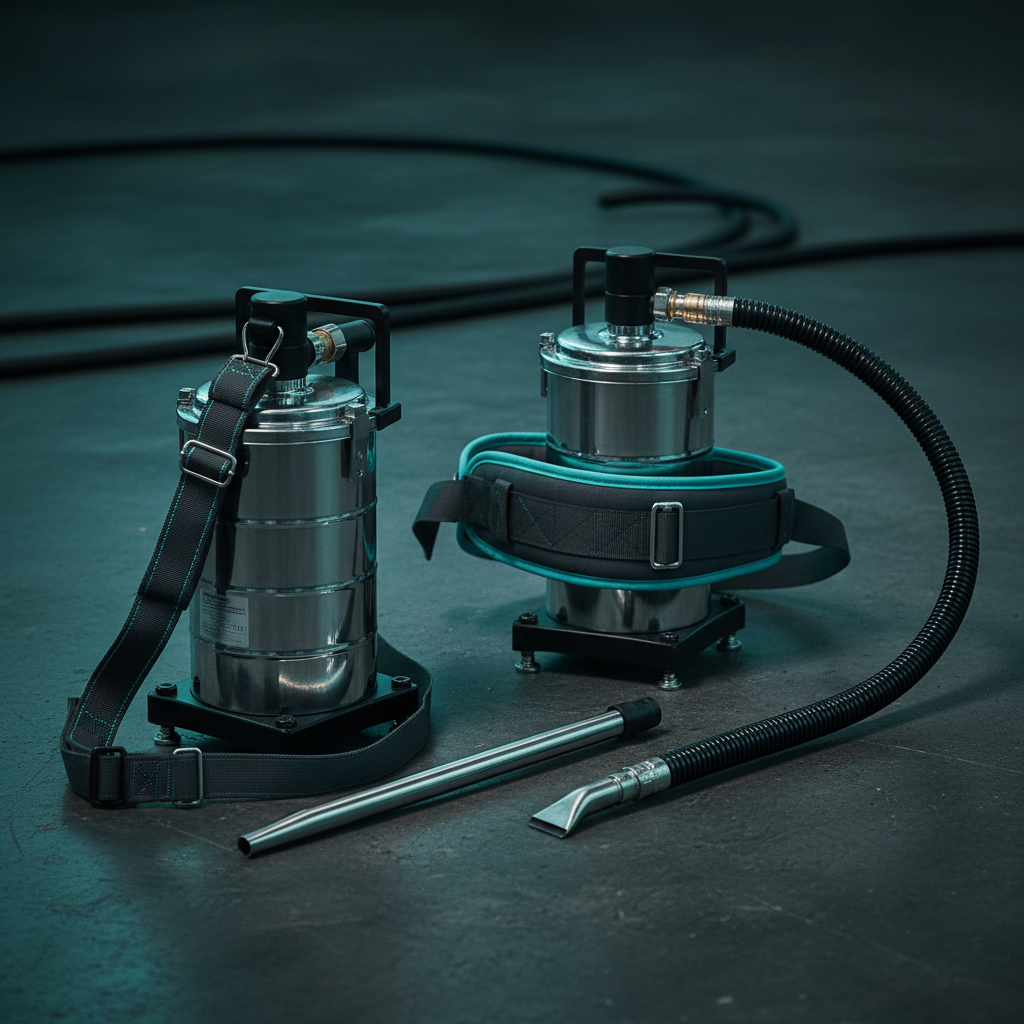
Portable and backpack air vacuums
Small canister, shoulder, and hip-carried units reach where drums cannot: platforms, walkways, vessel interiors, machine enclosures, and ladder access. Capacity and air consumption are both low. They trade volume for the ability to follow an operator into confined or elevated spaces on a short air whip.
Reaches elevated, confined, and enclosed spaces a drum unit can't.
This model draws the least compressed air in the lineup, frequently supplied from a nearby drop.
Small capacity suits spot cleaning, not bulk recovery.
Wet, dry, submerged recovery with pump-out
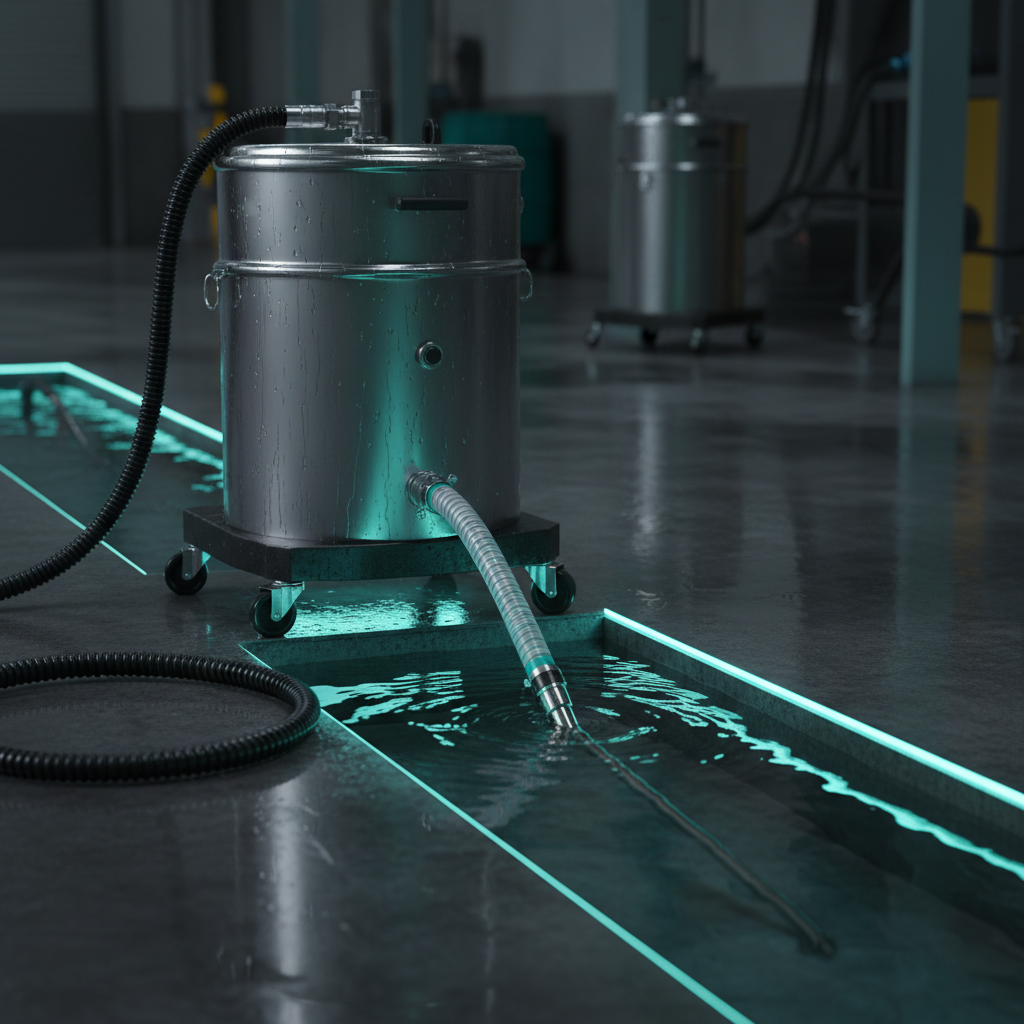
Units handle liquid, slurry, sludge, and dry material, with wet-capable filtration and an automatic shutoff to prevent overfill. Pump-out models add an air-driven discharge that pumps recovered liquid to a drain, tote, or tanker during recovery, so large liquid jobs run without stopping to empty the vessel.
Wet-capable filtration and overfill shutoff included.
Pump-out pushes liquid out via hose, enabling uninterrupted recovery.
Standard for sump, pit, and coolant recovery.
Multi-venturi high-lift heads
Multiple venturis in parallel deliver lift for dense material, heavy lifts, and long hose runs that exhaust a single venturi. Typical uses: metal shot, swarf, wet sludge, and recovery from distant pits or vessels. Air consumption scales with venturi count, so size the air supply first.
Produces higher suction for heavy substances and extended hose paths, including vertical lifts.
Handles heavy material that a single-venturi head only rattles.
Highest air consumption in the range; verify SCFM at the head.
Related: pneumatic vacuum conveyors
A vacuum conveyor applies the same venturi principle as process equipment, not a cleaner. It continuously moves product from a sack tip, drum, or bulk bag into a hopper, mixer, or reactor, discharging through a valve on a repeating cycle. Some heads handle both tasks. If material must arrive at a specific point on a cycle as part of the process, you're specifying a conveyor, not a vacuum cleaner.
Not the same: pneumatic vacuum generators
A vacuum generator in factory automation is a small inline device near tooling that pulls vacuum on suction cups for a robot to lift a part. It shares only the venturi principle: no vessel, hose, filtration, or debris. The products are often confused because search terms overlap. For part holding, you need a generator; for removing powder, chips, or liquid, you need a vacuum.
Pneumatic vs. Electric Industrial Vacuums
Electric industrial vacuums are cheaper to run and quieter. Pneumatic units go where electric motors can't and run as long as air is supplied. The comparison below is honest; operating cost is the line buyers usually discover later.
Attribute
Pneumatic (air powered)
Electric
Power source
The vacuum runs on compressed air at the head, usually between 60 and 100 psi. It requires no electric power at the unit.
An electric head needs a power cord, a motor, and a live circuit at every location it operates.
Hazardous locations
Once the bonding, grounding, and material specs are matched to the zone, this unit is the preferred option near flammable fumes or explosive dusts.
An electric alternative demands a motor and controls certified for the hazardous zone, increasing bulk and expense and frequently not offered in a portable form factor.
Duty cycle
Run time is continuous because no component inside the power head generates heat; only the available air supply and the drum capacity constrain operation.
Operation is capped by motor heat. Numerous workshop models carry intermittent duty ratings and stop when they overheat.
Operating cost
Cost is greater. Compressed air ranks among the priciest utilities per CFM, and the head consumes its full rated flow continuously while in use.
Lower operating cost. A motor spins a fan directly, avoiding the extra energy conversion step required with compressed air.
Noise
A loud high-frequency jet without a properly fitted exhaust muffler.
Lower and lower-pitched, mainly motor and fan noise.
Weight and portability
The setup is light: a drum-top unit comprises just a head, a clamp, and a drum already present on site, needing only a compressed-air connection.
An electric vacuum is heavier, with its motor, housing, fan, plus the cord that must be handled and a socket that must be located.
Maintenance
This power head contains no spinning electrical components. Motors, brushes, bearings, and cooling fans are not present in the power head. Instead, it works with a venturi and the necessary filter elements, seals, silencer, and tubing.
An electric power head adds a motor, bearings, brushes (if included), cooling fan, and cord, in addition to the identical filters and seals.
Where they excel
Applications by industry
The machine itself changes little across industries. Differences lie in area classification, material, liquid handling, and exhaust cleanliness requirements.
Chemical/petrochemical plants
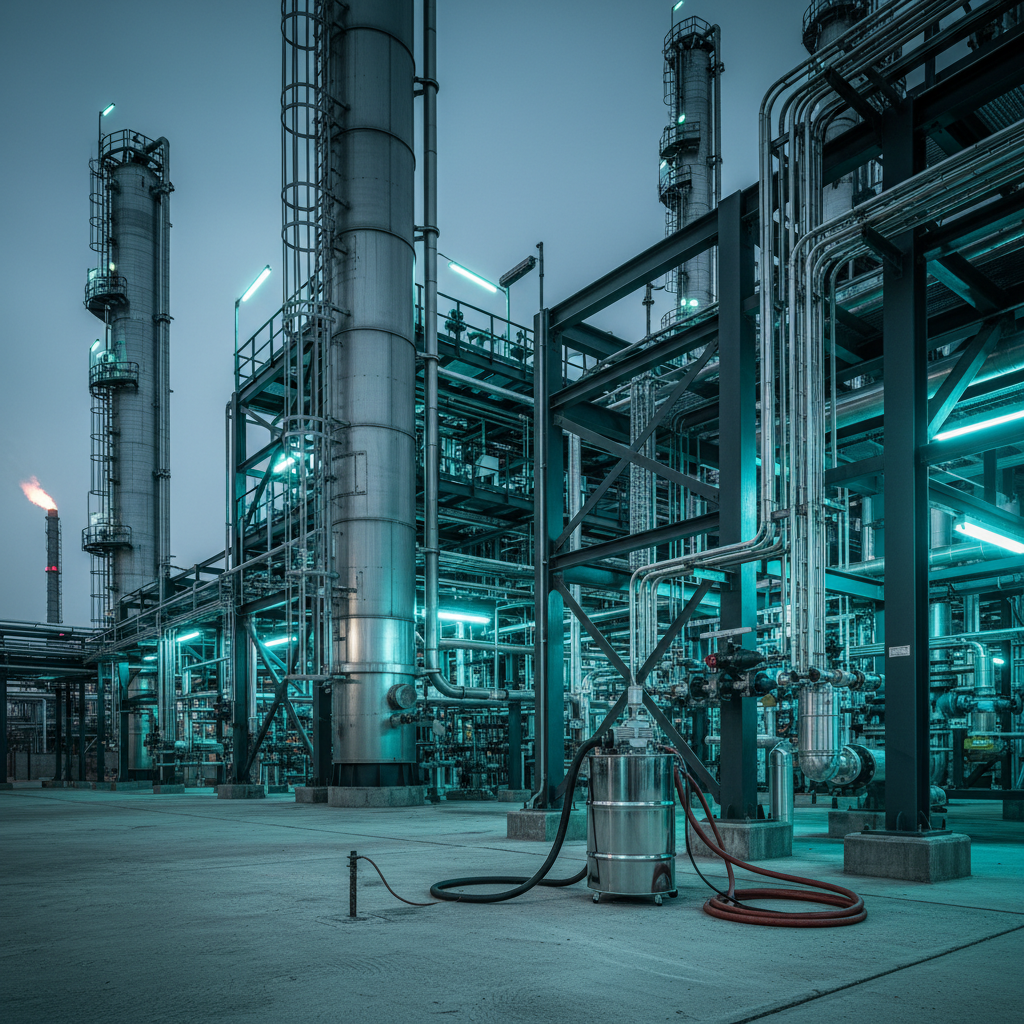
Process units are classified areas where corded electric vacuums are often unacceptable. Air-powered units handle catalyst, spills, product, and washdown water without introducing an electric motor into flammable vapour zones. Nothing overheats during extended turnarounds; the head is easily decontaminated and moved between units.
No electric motor enters the classified process area.
Runs continuously through turnarounds and shutdowns.
Handles dry spill and the subsequent washdown water.
Pharmaceutical/API powder handling
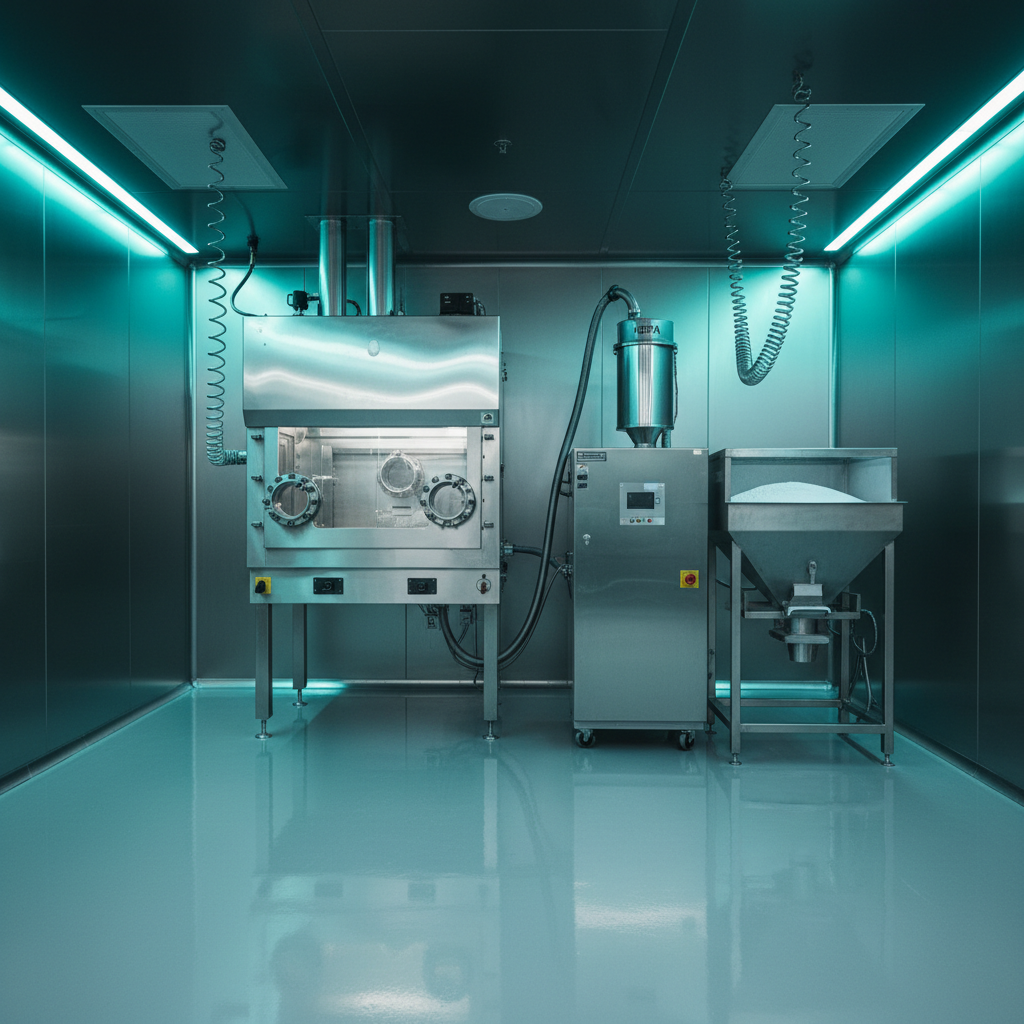
Dispensing, granulation, and tablet areas produce fine active powder that cannot be swept, blown, or exhausted into the room. Polished 316 stainless wipes clean and withstands cleaning agents; HEPA filtration keeps exhaust clean; an air-powered head avoids motor windings or cooling fans in controlled spaces.
Polished 304 or 316 stainless construction for cleaning and rapid changeover.
HEPA final filtration when exhaust returns to a controlled room.
Contains fine active powder, keeping it from spreading.
Food, grain, flour & combustible dust
Flour, sugar, starch, grain dust, and many other food powders are combustible. Housekeeping is the primary defense. Air-powered vacuums eliminate the electric motor; with conductive hose, tools, and a bonded ground path, they give static from moving dry powder a safe escape.
Eliminates the electric motor from combustible dust areas.
Static-conductive hose and bonded ground path as standard.
Wash-down capable, so one unit serves wet cleaning zones.
Metal chips and coolant recovery
CNC machining centres, screw machines, and grinders deposit chips, swarf, fines, and used coolant into sumps. A high-lift vacuum head extracts the weighty solids, while a pump-out version sends the reclaimed coolant back to a tank or filtration skid, rather than storing it in drums across the factory.
Paint/powder coating booths
Booth floors, grating, filter plenums, and overspray near a powder gun demand frequent cleaning in areas where solvent vapour or combustible powder is inherently present. Air power with bonding and grounding is the standard solution; a wash-down capable head withstands cleaning agents.
Foundries and metal powders
Hot sand, shot blast media, grinding fines, and metal powders are dense, abrasive, and sometimes reactive. Multi-venturi lift handles the weight; abrasion-resistant construction is specified. Metal powders introduce ignition and reactivity risks that must be addressed during specification.
Tank, sump, pit cleanout, and shipyards
Confined space and marine work involve long hose runs, distant vessels, liquid with solids, and no electricity at the operator's location. High-lift heads with pump-out are the typical choice, powered by a long air line instead of a long cord.
Getting specification right
Nine criteria that decide selection
Almost every complaint traces to one of these nine choices, made at purchase and lasting years. A head starved of air, a filter too coarse, or a drum too heavy to move are specification errors, not maintenance issues.
01
Material to recover
Start with what travels up the hose: fine powder, granules, chips, swarf, wet sludge, standing liquid, or a mix. Density determines lift, particle size sets filtration, and abrasiveness and chemistry dictate construction. All other decisions follow.
02
Area classification
From your process safety documentation, establish the area classification: Class I for flammable gases/vapours, Class II for combustible dusts. Match a specific model rated for that area; don't assume any air-powered unit is automatically acceptable.
03
Available air supply
Make sure SCFM and psi are measured at the drop where the vacuum will be placed, not at the compressor. If pressure falls below the rating, both lift and airflow degrade, making the unit appear underpowered. Also check what other equipment draws from that same header simultaneously.
04
Lift against airflow
Lift pulls heavy material and moves it a distance. Airflow clears large volumes of light material fast. Decide which the job requires, because selecting by one metric and judging by the other causes most disappointment.
05
Filtration level
Match media to particle: cloth bag or coarse cartridge for chips and debris, pleated cartridge at correct efficiency for fine powder, and HEPA final where exhaust returns to occupied or controlled spaces. Specify filter area generously.
06
Drum sizing and handling
A full 55 gallon drum of wet sludge cannot be moved by one person. Choose 30 or 55 gallon based on how the full vessel leaves the area. Specify the dolly, tipper, or lifting arrangement with the head, not later.
07
Wet, dry, or pump-out
Dry-only units are simplest. Wet/dry adds a shutoff and wet-capable filtration. Pump-out enables continuous liquid discharge, turning hours of drum changes into a single uninterrupted job. Decide before selecting.
08
Hose length and diameter
Hose diameter normally ranges from roughly 1.5 to 3 inches. A wider bore handles larger particles with lower resistance but demands more airflow to maintain transport velocity. Each additional foot of hose and each bend reduces suction; therefore, specify only the shortest run that the job actually requires.
09
Noise limit
Establish the noise limit before selecting, then request the sound level with muffler fitted. Addressing noise during specification is straightforward; fixing it post-commissioning often means buying a different head.
On the data sheet
Key Specifications and Their Meaning
A pneumatic vacuum data sheet is short, but every line has a plant-floor consequence. Read lift and airflow together, air consumption against actual header delivery at the drop, and filtration against the finest particle you'll recover.
Three numbers to send a supplier
The SCFM and psi supplied at the drop point where the vacuum operates.
The type of material, its condition, and approximately the quantity handled per shift.
The hose length and internal diameter, plus the vertical rise from the nozzle to the collection vessel.
Specification
What it tells you
Typical range/note
Compressed air consumption
The running cost and the supply capacity required.
Air consumption is generally in the tens of SCFM; small portable heads sit at the lower end, and multi-venturi models consume significantly more. The head draws its full rated flow nonstop while running.
Head supply pressure
The pressure the venturi requires for rated performance.
Pressure between 60 and 100 psi is the norm. Take drop readings rather than compressor values. When supply falls below the rating, suction and flow decline together, and the unit may seem defective.
Inlet/hose diameter
This depends on the biggest particle that must travel through the hose and the total resistance of the hose pathway.
Typical hose diameters fall between 1.5 and 3 inches. A larger bore moves more material with lower pressure loss, yet asks for more airflow to sustain proper conveying speed.
Water lift
This indicates the weight of the material the head can lift and the distance it can move it.
Measured in inches of water or inches of mercury with the inlet sealed. This figure is critical when dealing with dense substances and extended or vertical hose runs.
Hose airflow
How fast a volume of light material clears.
Specified as CFM at the hose end while material moves. Interpret alongside lift. A filter that is loading reduces this value well before the filter appears visibly dirty.
Filtration
What stays in the vessel and what exits the exhaust.
Select a cloth bag, a pleated cartridge, or a cartridge plus a HEPA final stage. Match medium to particle, and specify filtering area instead of frequent cleaning.
Sound level, muffled
Whether the unit meets the noise limit.
Request the noise level with the muffler installed, because the venturi exhaust without it produces a piercing, high-frequency jet. A broken muffler is a defect, not merely a nuisance.
Construction material
Cleanability, corrosion resistance, and abrasion life.
Choose carbon steel for general applications, aluminum when weight is a concern, and polished 304 or 316 stainless steel for pharmaceutical, food-grade, or corrosive environments.
Conductive hose and bonding
Provides a path to earth for static from moving dry powder.
Use conductive hoses, wands, and nozzles together with a bonding strap linking the vessel to a verified grounding point. Make continuity testing a regular practice, not just a one-time setup step.
Drum compatibility
Whether the head fits your existing vessels.
Check that the clamping band and seal fit your 30- or 55-gallon drum. At the same time, choose the dolly, tipper, or lifting setup.
Liquid pump-out
Whether recovery can continue after the vessel fills with liquid.
Pneumatically powered ejector sends recovered liquid through flexible hose to drain, tote, or tanker. Verify the discharge head and how much hose you need to cover the liquid’s path.
In service
Commissioning and six maintenance habits
No motor means maintenance focuses on air quality, filtration, seals, and the hose. Six habits address nearly every reported performance drop; five take a minute each.
Installation and Commissioning
1Place an FRL unit at the compressed air drop; flush the airline before attaching the head; then adjust the control to the specified pressure.
2Verify that the air line's diameter and length can sustain that pressure at maximum flow, and identify what other devices pull from the same header during operations.
3Place the head onto the drum ensuring the lid gasket is intact, completely tighten the band clamp, and check that the filtration grade matches the material specification.
4For combustible dust or flammable liquid operations, install static-dissipative tubing and instruments, connect a ground cable to a confirmed earth terminal, and test the full electrical path.
5Operate the unit using clean substances, ensure the silencer is attached, and note the supply pressure, lift, and operator’s sense of suction. This record provides a baseline for later comparison.
Supply the head with dry, clean air via a filter-regulator.
Compressed air often contains water, pipe scale, and compressor oil. These contaminants clog a venturi and collect in the filtration. Install a filter-regulator at the drop, drain its bowl on a schedule, and adjust the regulator to the rated pressure, not whatever the header happens to supply.
Treat the muffler as an integral machine component.
The muffler makes the unit tolerable to work near; a clogged one restricts exhaust and reduces performance. Inspect for packing loss and blockage, clean or replace on schedule, and never run a head with the muffler removed just because it was loud.
Inspect the venturi for wear and clogging.
The power head has no moving parts, but the nozzle and throat are precision restrictions. Abrasive carry-over slowly enlarges them; debris or scale can partially block them. Either causes lost lift at constant supply pressure. Inspect per the manual and whenever performance drops despite clean filters.
Clean or replace filters on schedule, not by appearance.
A filter loaded with fine powder starves airflow long before it looks dirty; operators often blame the head. Clean or change elements on interval, inspect seals and housing gaskets each time, and keep spares for the powders you handle.
Examine the drum’s gasket and the lid’s sealing ring whenever you change drums.
The head can only pull vacuum on a sealed vessel. A flattened, split, or missing gasket, a dented rim, or a loose band clamp all mimic a weak machine at the hose. Check this first when suction drops without obvious cause.
Check the hose and grounding path together.
Look for wear-through, collapsed reinforcement, and cuts at cuffs. On conductive hose, confirm continuity from nozzle through hose, head, and vessel to ground. A conductive hose with a broken path is worse than useless because it is trusted.
Common questions
Pneumatic vacuum FAQ
What exactly is a pneumatic vacuum?
A pneumatic vacuum is an industrial vacuum cleaner powered by compressed air instead of electricity. Compressed air is fed to a venturi, also called an ejector, inside the power head. There it passes through a nozzle at high velocity and drags the surrounding air along with it, which pulls a vacuum on the recovery vessel and the hose. There is no electric motor, no cord and no electricity at the vacuum itself, and the power head has no moving parts to wear out.
A venturi vacuum head produces suction, yet it functions without any internal motion.
Compressed air is forced through a converging nozzle inside a larger throat. The air leaving the nozzle travels far faster than the air around it, and that high-velocity stream entrains the slower air beside it and carries it out through the exhaust. Air leaves the sealed recovery vessel faster than it can leak back in, leaving a pressure difference, and atmospheric pressure pushes material up the hose. Giovanni Battista Venturi described the effect in the late 1700s, and air ejectors on the same principle have moved air, steam and vapour in industry since.
Why choose a pneumatic vacuum over an electric industrial vacuum?
Four reasons drive most purchases. Hazardous locations, where an electric motor is unwelcome near flammable vapours or combustible dust. Wet and washdown areas, where the unit can be hosed down and no motor or winding has to stay dry. Continuous duty, since no motor can overheat and run time is limited only by the air supply. Maintenance, because the power head has no armature, brushes, bearings or fan to replace. The trade-off is operating cost: compressed air is an expensive utility.
Do Class I and Class II hazardous locations allow Pneumatic Vacuums to be used?
They are the usual choice there, but suitability belongs to the specific unit and area classification, not to the technology as a whole. Removing the electric motor removes one ignition source; the rest must be engineered: static-conductive or static-dissipative hose and attachments, a continuous bonding and grounding path from nozzle through hose, head and vessel to a proven ground point, and materials suited to what is being recovered. Confirm the area classification against your own electrical and process safety documentation, then confirm in the manufacturer's documentation for that model that the unit is rated for it.
How much compressed air does a pneumatic vacuum consume?
Typical consumption is tens of SCFM at roughly 60 to 100 psi supply, with small portable heads at the low end and high-lift multi-venturi heads at the top of that range or above. Read the figure at the pressure you can actually deliver at the head, not at the compressor; a long or undersized air line starves it. Size the supply with margin. A head fed below its rated pressure loses lift and airflow and looks like a weak vacuum when the air line is the real fault.
Can a pneumatic vacuum handle liquids and sludge?
Achieving this requires a unit built for the purpose. Models intended for wet and dry conditions employ a float or cutoff that halts collection before the vessel fills, along with filtration media that resist collapse when saturated. Submerged-recovery designs build on this with a pump-out: an air-driven discharge that routes the collected liquid via a hose to a drain, tote, or tanker while collection continues, so the operation need not pause every time a drum is full. This configuration is standard for cleaning tanks, sumps, and pits, and for recovering coolant.
What is water lift, and how does it differ from airflow?
One key metric is water lift, recorded in inches of water or inches of mercury, indicating the pressure differential achievable at a sealed intake. It reveals the weight and distance a material can be moved, be that vertically or along extended hose. Airflow, measured in CFM at the hose, is the air volume passing through once material starts moving and determines how rapidly light debris in bulk can be cleared. Heavy substances, lengthy hose runs, and compact nozzles call for lift. Collecting large quantities of lightweight waste demands airflow. Frequent missteps in selection arise from examining only one figure and overlooking the other.
How loud does a pneumatic vacuum get?
An unmuffled venturi exhaust is a loud, high-frequency hiss, because it is a jet of compressed air discharging to atmosphere. A muffler on the exhaust brings that down substantially and is standard equipment, not an accessory. If you have a boundary or in-plant noise limit, establish it before selection, ask for the sound level of the specific model with its muffler fitted, and treat a missing or damaged muffler as a fault to be fixed rather than an inconvenience. Noise is usually the first thing operators complain about and the easiest to design out.
Do pneumatic vacuums require grounding and bonding?
The presence of combustible dust or flammable liquid makes it essential, and this is a primary reason for specifying this vacuum design. Conveying dry particulate through a tube accumulates electrostatic charge. Grounding and bonding provide a safe earth path for that charge, preventing buildup and sparking. This translates into using a hose that conducts static, not basic plastic, along with conductive wands and tips, a bonding cable from the container to a verified earth, and performing a regular continuity test on the complete circuit, not a one-time check during startup.
What filtration is needed for fine powder?
Select filters based on the particle, not the vacuum unit itself. For chips, granules, and ordinary debris, a fabric bag or coarse filter cartridge is sufficient. Substances like flour, pigment, and active pharmaceutical ingredients are fine powders; they penetrate coarse media and exit with the airflow. Consequently, the system needs a pleated cartridge with adequate efficiency, and typically a HEPA final stage when the discharge is directed into an occupied or controlled space. Increase filter surface area instead of depending on regular cleaning, since a loaded filter restricts airflow far sooner than it appears dirty.
Does 'pneumatic vacuum conveyor' equal 'pneumatic vacuum'?
These two are akin but serve distinct purposes. A vacuum cleaner draws in spillage, debris, or liquid into a tank that is eventually emptied. Pneumatic vacuum conveyors are considered process equipment. They harness the same venturi principle, or a standalone vacuum pump, to continuously transport material from a drum, sack tip, or bulk bag up to a hopper, mixer, or reactor, and then release the load through a valve in cycles, avoiding any tipping. Certain venturi heads can handle both roles. When the material must land at a designated spot on a set repeat, the requirement is a conveyor.
Do 'pneumatic vacuum generator' and 'pneumatic vacuum cleaner' denote identical devices?
No, and the two terms cause regular confusion. A vacuum generator or ejector in factory automation is a small inline device, often a compact block mounted near the tooling, that pulls vacuum on suction cups so a robot or gripper can pick up a part. It shares the venturi principle and nothing else: no recovery vessel, no hose, no filtration, no debris. A pneumatic vacuum as described on this site is a cleaning and recovery machine. If you need cups to hold a part, you want a generator. If you need to clear powder, chips or liquid, you want a vacuum.
Talk to someone
Get a quote for the right pneumatic vacuum.
Selecting a pneumatic vacuum is describing a job, not picking a part number. Tell us what material goes up the hose, the air available at the drop, and the work area, and your inquiry reaches a specialist who sizes these daily.
Material: powder, granules, chips, sludge, standing liquid, or mix.
The SCFM and psi available at the drop, along with the other equipment that draws from that same header.
Area classification, including presence of combustible dust or flammable liquid.
Wet, dry, or continuous pump-out.
The hose length and internal diameter, plus the vertical rise from the nozzle to the collection vessel.
Filtration needed, including any HEPA exhaust requirement.
Your preferred drum style, the method for moving a full drum out of the workspace, and any noise constraints.